Heavy-Duty Bucket Elevators for Bulk Material Handling
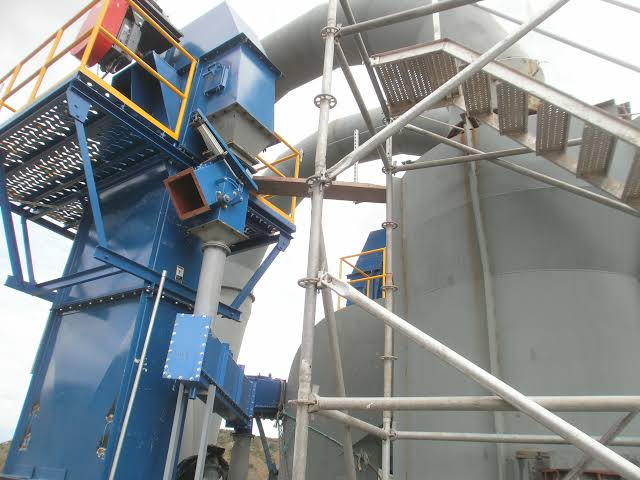
Bulk material handling is one of those behind-the-scenes operations that rarely gets attention until something goes wrong, and when it does, the entire production line feels it. At the center of many of these systems sits the bucket elevator, a piece of equipment tasked with the demanding job of lifting tons of raw material vertically, hour after hour, often in harsh and unforgiving conditions. For industries like cement, mining, and aggregate processing, a standard elevator simply will not cut it. What these operations need is a heavy-duty bucket elevator built specifically to handle abrasive materials, extreme temperatures, and continuous high-volume throughput without breaking down.
Why Heavy-Duty Design Matters
Not all bucket elevators are created equal, and the difference becomes obvious the moment you introduce dense, abrasive, or high-temperature materials into the mix. A lightweight system designed for grain or plastic pellets will wear out quickly if asked to move crushed limestone or cement clinker day after day. Heavy-duty bucket elevators are engineered with reinforced buckets, thicker steel casings, and more robust chains or belts specifically to withstand this kind of punishment. Manufacturers such as Cementl understand this distinction well, since much of their engineering focus centers on building equipment that can survive the brutal realities of cement production, where dust, heat, and constant mechanical stress are simply part of daily operation.
Key Features That Define a Heavy-Duty Bucket Elevator
When evaluating a heavy-duty bucket elevator, a few features consistently separate industrial-grade systems from lighter commercial ones. Bucket material and thickness matter enormously, since manganese steel or hardened alloy buckets resist abrasion far better than standard steel. Drive systems also need to be sized appropriately, with heavier chains and reinforced sprockets capable of handling continuous loads without stretching or snapping under pressure. Casing construction is another critical factor, as thicker steel walls protect internal components from both material impact and external environmental exposure. Beyond the physical components, a well-designed bucket elevator also incorporates safety features like backstops to prevent reverse rotation and speed sensors to catch mechanical issues before they escalate into costly failures. Cementl has built its equipment lineup around these exact principles, recognizing that cutting corners on any one of these features can compromise the entire system.
Common Applications in Bulk Material Handling
Heavy-duty bucket elevators show up across a wide range of industries, though cement production remains one of the most demanding applications. Moving raw materials like limestone, clay, and clinker through various stages of processing requires equipment that can operate continuously without frequent shutdowns for repair. Mining operations rely on similarly rugged systems to transport ore and aggregate materials, often in environments with significant dust and moisture exposure. Power plants handling coal and biomass also depend on heavy-duty bucket elevators to keep fuel supply chains moving efficiently. Across all these applications, the common thread is a need for equipment that can handle abrasive, heavy, and sometimes hot materials without constant intervention, which is precisely why so many plant engineers turn to specialized manufacturers rather than off-the-shelf solutions.
Choosing the Right System for Your Operation
Selecting a heavy-duty bucket elevator is not something to approach with a one-size-fits-all mindset. Throughput requirements, material characteristics, vertical lift height, and environmental conditions all play a role in determining the right configuration. A facility processing cement clinker will have very different needs than one handling coal or grain, even though both might technically fall under the heavy-duty category. Working with a manufacturer that takes the time to understand these nuances, rather than pushing a generic solution, tends to produce far better long-term results. Cementl has earned a strong reputation in this space precisely because their engineering team focuses on tailoring each bucket elevator to the specific demands of the client’s operation, rather than relying on standardized designs that may not hold up under real-world conditions.
Final Thoughts on Heavy-Duty Bucket Elevators
Bulk material handling places enormous demands on equipment, and there is little room for error when a production line depends on continuous vertical transport of heavy, abrasive materials. A heavy-duty bucket elevator built with the right materials, robust drive components, and thoughtful engineering can mean the difference between years of reliable operation and constant, costly downtime. For companies serious about long-term efficiency, investing in a properly specified bucket elevator from an experienced manufacturer like Cementl is not just a purchasing decision but a strategic one. If your operation is ready to move beyond frequent breakdowns and inconsistent throughput, it may be time to explore what a truly heavy-duty solution can bring to your bulk material handling process.